- Products
- Workshop equipment and tools
- Pumps
- Chemical pumps
Chemical pumps
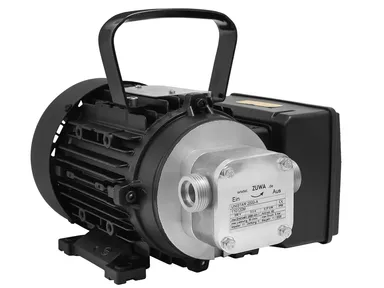
A chemical pump is chosen first by material: the body, diaphragms, seals and valves must withstand the specific liquid, concentration and temperature. That is why this category has the same pump type in several materials, from polypropylene and PVDF to acid-resistant stainless steel and PTFE seals.
For emptying a drum or container, a drum pump with a pump tube is used, attached to the pump tube opening of the drum with a bung nut or to a wall bracket, and the motors are also available ATEX-approved. For thinners and solvents there are acid-resistant stainless steel drum pumps with PTFE seals, and for flammable liquids a drum pump with a flame arrester and grounding cables. Dirty liquids or liquids containing solids are transferred with a diaphragm pump. In fixed installations, a magnetic drive centrifugal pump works without a shaft seal, but it is not self-priming and does not tolerate particles.
For fuels, choose a fuel pump, and for AdBlue, a urea pump.
35 products